Why cabinet shops keep coming back to modern edge solutions
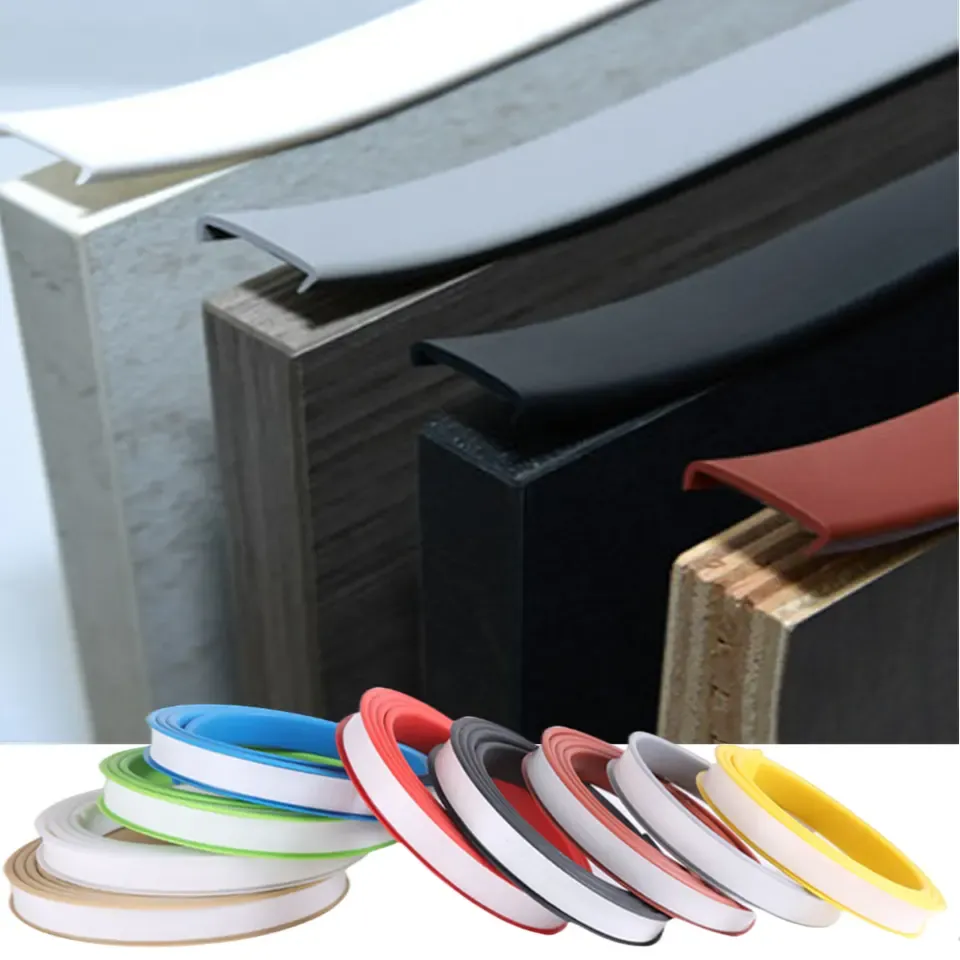
If you’re evaluating how to finish panels cleanly and profitably, the humble edge banded strip has quietly evolved. In fact, over the past three years I’ve watched shops move from commodity tape to co-extruded, color-stable bands that actually survive jobsite abuse. And yes, that matters when end users slam cabinet doors (they do) and cleaners use harsher chemicals than they admit.
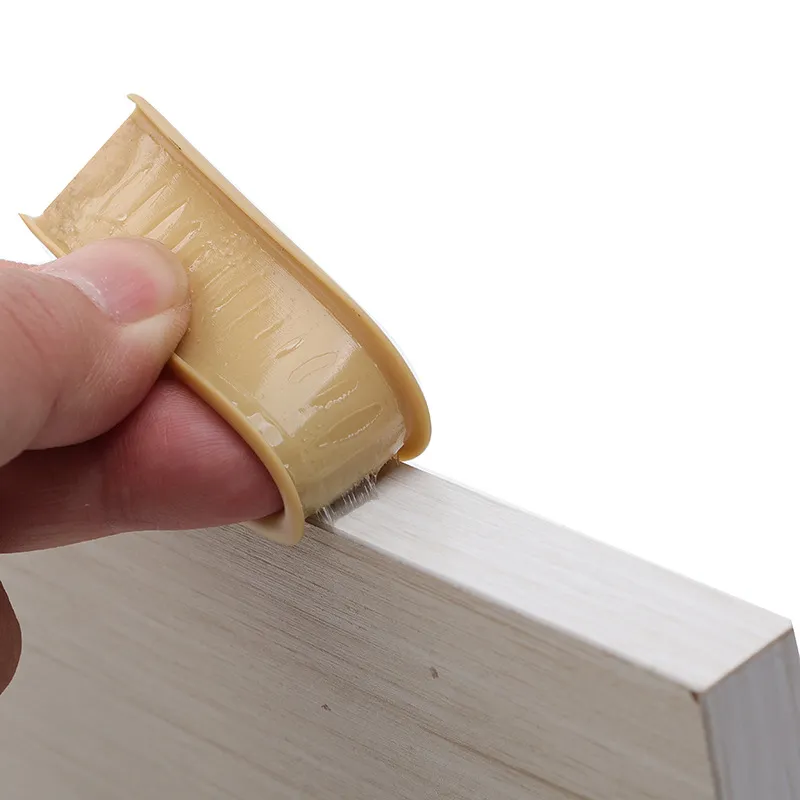
What’s inside: materials and process (short version)
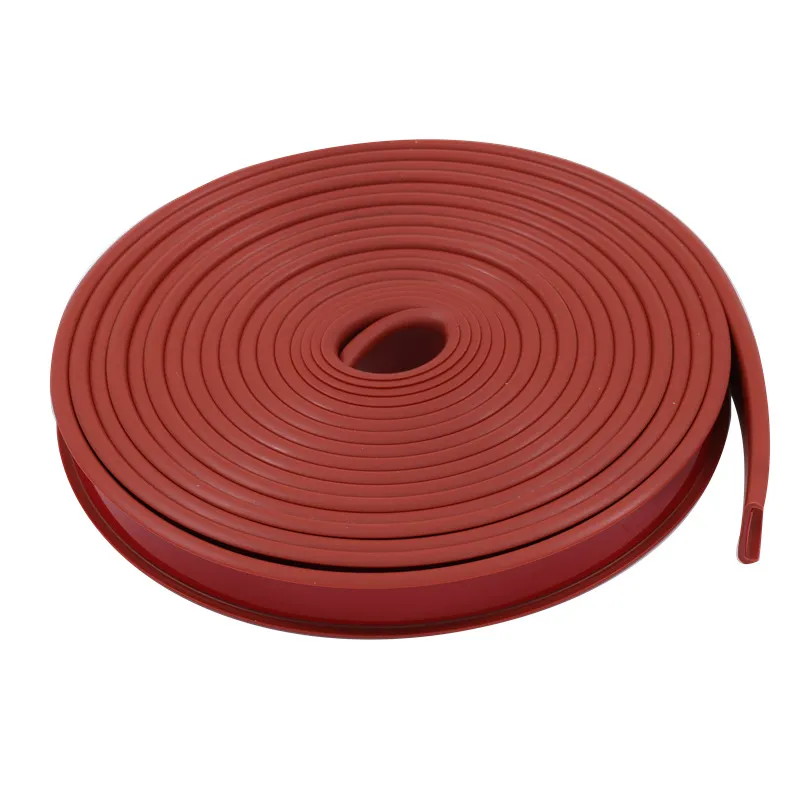
Origin matters: this line comes out of Wangshigong Industrial Zone, Wei County, Xingtai, Hebei—a cluster that’s gotten very good at tight-tolerance extrusion. The product family covers PVC (workhorse), TPE (impact-friendly), and Silicone (sealing edges; niche but useful near sinks).
- Compounding: stabilized PVC/TPE resin with pigments and UV package.
- Co-extrusion: base layer + decorative/top layer; grained embossing optional.
- Primer coating: adhesion promoter tuned for EVA or PUR hotmelt lines.
- Digital color match: ΔE targets set against panel decor libraries.
- Topcoat/UV: scratch and stain resistance where specified.
- Slitting & QC: width/height control, coil tension, lot traceability.
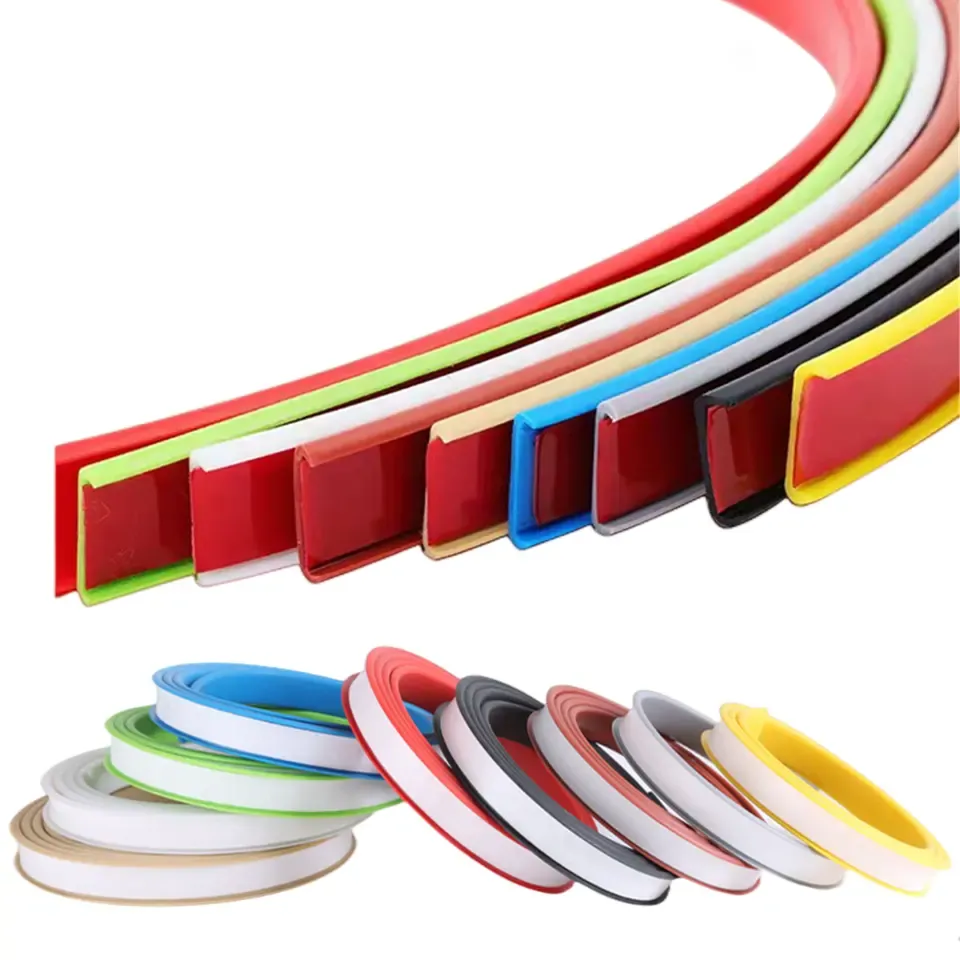
Technical specs (real-world, not brochure fluff)
| Parameter |
PVC |
TPE |
Silicone |
| Thickness |
0.4–2.0 mm |
1.0–2.5 mm |
1.5–3.0 mm |
| Width |
16–65 mm (custom up to 100 mm) |
16–65 mm |
Up to 60 mm |
| Heat resistance |
≈85–95°C (EVA/PUR) |
≈80–90°C |
≈120°C |
| Cold crack |
≤−20°C |
≤−30°C |
≤−40°C |
| Adhesion (ASTM D3359) |
4B–5B |
5B |
5B |
Test snapshots: peel ≥15 N/25 mm on MDF with PUR; ΔE ≤1.0 after 200 h ISO 4892 UV; stain class 1–2 on coffee/ethanol (EN 12720-like), real-world use may vary. Service life: 8–12 years indoors, assuming typical cleaning chemicals.
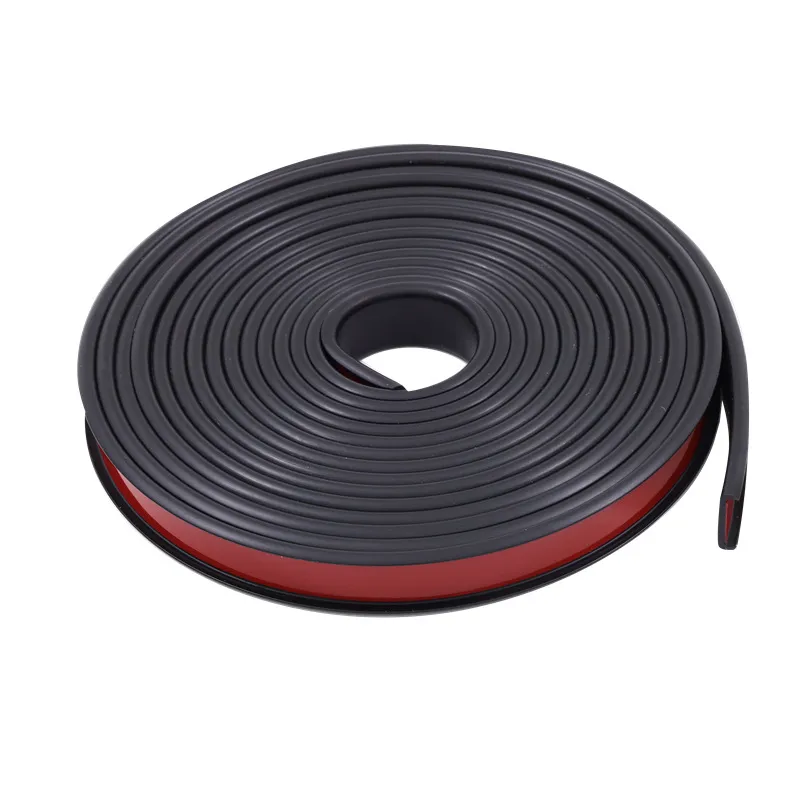
Where it’s used (and why shops care)
- Kitchens and baths (humidity, heat from appliances).
- Office furniture and retail fixtures (traffic + cleaning cycles).
- Healthcare casework—TPE and Silicone edges help with impact and sealing.
Advantages I’ve seen: fewer returns for edge lift, better color match to mainstream decors, and smoother trimming—especially on PUR lines running faster than 18 m/min. Many customers say the primered surface feels “stickier” (in a good way) during setup, which reduces first-piece scrap.
Vendor comparison (quick, imperfect, but useful)
| Vendor |
Strengths |
Lead Time |
Certs |
Notes |
| QZSeals (this line) |
Co-extruded PVC/TPE; tight color match; PUR-ready primer |
10–15 days |
RoHS, REACH, low VOC, optional CARB alignment |
Balanced price/performance |
| Imported A-brand |
Huge decor library; excellent UV topcoats |
3–6 weeks |
EN, ISO suites |
Premium pricing |
| Local distributor brand |
Fast delivery, small MOQs |
2–5 days |
Basic RoHS |
Watch batch-to-batch color |
Customization, installs, and quick case notes
Customization: RAL/NCS color matching (ΔE ≤0.8 typical), woodgrain prints, gloss from 5–90 GU, embossed textures, pre-glued options, widths up to 100 mm for thick tabletops. EVA or PUR compatible; most shops still run EVA, but PUR is gaining—honestly, the bond line looks cleaner.
Case snapshots: a mid-size kitchen OEM cut rework by 27% after switching to edge banded PVC with upgraded primer; a clinic millwork project used TPE to soften corner impacts; a hotel refresh chose Silicone near wet bars to resist wicking. Feedback? “Trim like butter,” one operator told me—color stability after six months also checked out.
Compliance, testing, and what to ask your supplier
- Standards/certs: REACH, RoHS, low-VOC; align with EN 14322/EN 438 panel use; UL 94 HB available on request.
- Testing to request: ASTM D3359 adhesion, ISO 4892 UV, ISO 178 flex, EN 12720 stain, formaldehyde compliance (CARB/EPA TSCA for panel system).
- Ask for peel data at both 20°C and 40°C; verify primer compatibility with your hotmelt; confirm batch ΔE and coil-length tolerances.
Citations:
- EN 14322:2017 – Wood-based panels – Melamine faced boards.
- EN 438 / ISO 4586 – High-pressure decorative laminates (context for surface durability).
- ISO 4892 – Plastics — Methods of exposure to laboratory light sources.
- ASTM D3359 – Standard Test Methods for Rating Adhesion by Tape Test.
- RoHS Directive 2011/65/EU and REACH Regulation (EC) No 1907/2006 compliance guidance.